Custom Software Development · Manufacturing
Custom Manufacturing Software Development
OEE, predictive maintenance, and quality software built from live machine data instead of monthly spreadsheet exports.
NDA on request · Free, no-obligation estimate · Reply within one business day
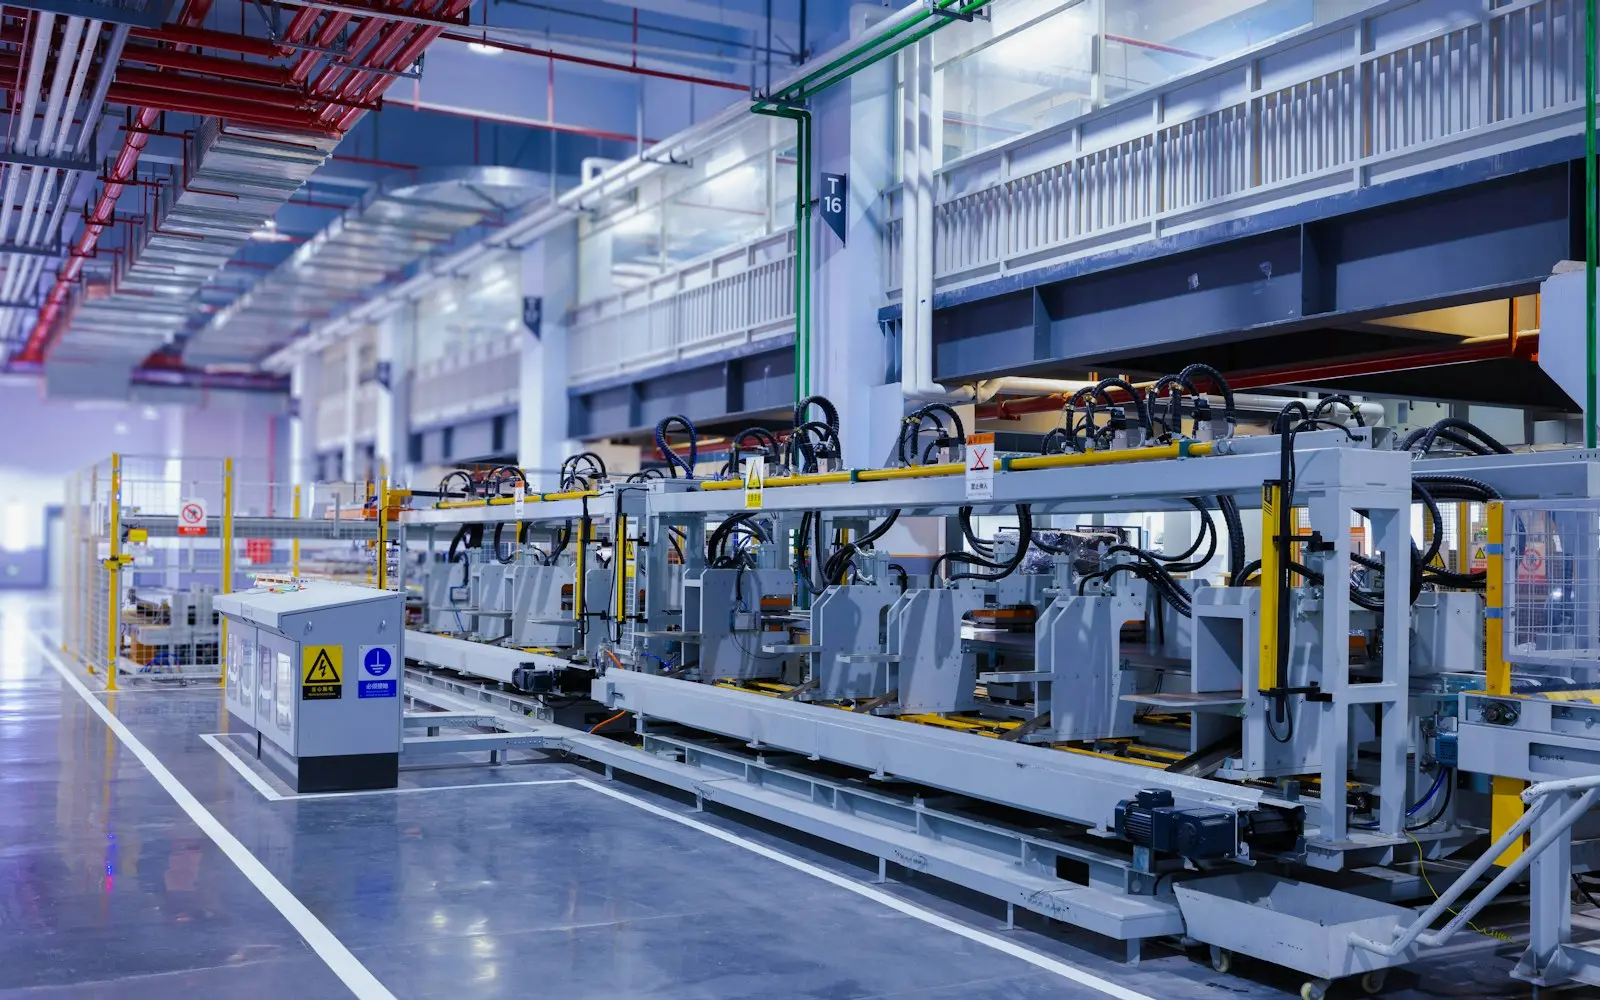
A plant manager who wants to know overall equipment effectiveness usually gets an answer built from a spreadsheet someone updates at the end of the month, by which point the downtime it's measuring has already cost real production. Getting that number in near real time means pulling machine state data directly from PLCs on the floor, and doing that across a mix of Siemens, Allen-Bradley, and older equipment means normalizing several incompatible data formats into one picture of uptime, speed, and quality.
We build the software layer that sits between machine data and the decisions a plant runs on: OEE calculation and downtime tracking sourced from PLC and SCADA systems, predictive maintenance models trained on sensor and failure history once that history is usable instead of scattered across paper logs, and statistical process control that captures a measurement at the point of production rather than transcribed later from a checksheet. Digital work instructions stay synced to the current engineering revision, so an operator on the floor is never working from a printed sheet that's already been superseded.
This sits alongside, not inside, the plant's existing ERP: we connect to SAP, NetSuite, or Epicor rather than duplicating financial or inventory data the ERP already owns, focusing custom development on the machine-level and quality data those systems were never built to capture.
The problem
What makes manufacturing projects different
OEE calculation needs to normalize incompatible PLC data
A stopped machine looks different in a Siemens PLC log than in an Allen-Bradley one, and calculating overall equipment effectiveness across a mixed-vendor floor requires normalizing that data into one consistent uptime and speed metric.
Predictive maintenance needs usable history, not just more data
Most plants start with years of maintenance logs that are unstructured or inconsistent rather than clean, labeled failure records, and a predictive model trained on that raw history first needs the data cleaned and structured before it's useful.
Statistical process control drifts without point-of-production capture
Measurement data recorded on a paper checksheet and entered into a system later loses the timing precision that lets a control chart catch a trend before it produces defective parts, so capture needs to happen at the machine, not after the shift.
Digital work instructions can go stale the moment a revision changes
An engineering change issued mid-shift needs to reach every workstation's instructions instantly, or operators keep following an outdated paper revision that's still sitting at the station.
Supplier quality scorecards span systems with no shared identifier
Incoming inspection results, warranty claims, and purchasing records usually live in three separate systems, and building a supplier scorecard means reconciling them without a common part or supplier ID to join on.
Scope
Features we commonly build
OEE calculation and downtime tracking
Machine state data pulled from PLC and SCADA systems across mixed vendors, normalized into a consistent overall equipment effectiveness metric.
Predictive maintenance alerts
Failure prediction models built on cleaned sensor and maintenance history, flagging a likely failure before it causes unplanned downtime.
Digital work instructions
Instructions synced to the current engineering revision at every workstation, replacing printed sheets that can fall out of date mid-shift.
Statistical process control charting
Measurement data captured at the point of production, feeding control charts that catch a drift before it produces out-of-spec parts.
Supplier quality scorecards
Incoming inspection, warranty, and purchasing data reconciled into a per-supplier scorecard despite living in separate source systems.
Andon-style line alerting
Line stoppage alerts routed to the correct supervisor automatically, replacing a physical andon cord with a targeted digital notification.
ERP and MES integration layer
A connection layer linking existing ERP, MES, and quality systems, so custom development adds machine-level capability without duplicating what those systems already own.
Real-time production scheduling
Scheduling logic that reacts to actual machine availability rather than a static plan, adjusting when a machine goes down unexpectedly.
Compliance and standards
- ISO 9001 process documentation support
- IATF 16949 supplier quality alignment
- OSHA recordkeeping
Common integrations
- OPC UA-connected PLCs
- Ignition SCADA
- existing SAP/NetSuite/Epicor ERP
- existing QMS
- barcode/RFID scanners
Approach
How we run these projects
We start on the floor, connecting to one production line's PLCs or SCADA system first and validating that the OEE and downtime data the new system reports matches what operators and supervisors already know is true, before extending to the rest of the plant. That validation step catches data normalization errors while they're still cheap to fix.
Predictive maintenance work starts with a data audit: cleaning and structuring the plant's existing maintenance history before any model gets trained on it, since a model built on inconsistent labels will look accurate in a demo and fail in production. Every integration with the existing ERP or MES is scoped to avoid duplicating a system of record the plant already trusts, and your team retains the codebase and infrastructure from the first commit.
Typical stack
Related solutions
Systems in this space
- System IntegrationConnecting the CRM, ERP, billing, and internal systems you already run, so data moves between them without a person copying it by hand.
- BI & Reporting DashboardsReporting built on one data model instead of five spreadsheets, with dashboards fast enough to stay useful against years of history.
- Internal Tools & Admin DashboardsBack-office software that lets your team look up, edit, and act on production data safely, replacing the spreadsheet or the direct database query.
FAQ
Frequently asked questions
How do you calculate OEE from machines running different PLC brands?
We build a normalization layer that reads machine state from each PLC or SCADA system in its native format and translates it into a consistent set of uptime, speed, and quality metrics, so a Siemens-controlled line and an Allen-Bradley-controlled line report OEE the same way.
Can predictive maintenance work without years of clean sensor history?
It needs some usable history to train against, but most plants have more raw data than they realize in maintenance logs and sensor readings; the first phase of the project typically focuses on cleaning and structuring that history before any model gets built on top of it.
How do digital work instructions stay in sync with engineering changes?
Instructions are pulled from a central revision-controlled source at the moment an operator views them, so an engineering change published mid-shift reaches every workstation immediately rather than waiting for someone to reprint and redistribute paper copies.
Does this replace our existing ERP or integrate with it?
It integrates with your existing ERP rather than replacing it. Custom development focuses on machine-level data (OEE, predictive maintenance, quality) that most ERP systems were never built to capture, while the ERP stays the system of record for financials and inventory.
How long does it take to build a custom manufacturing quality and OEE system?
A focused system covering OEE tracking and digital work instructions for one production line typically takes a few months, with predictive maintenance and supplier scorecards adding time depending on how much historical data needs cleaning first.
Can supplier scorecards combine data from separate inspection and purchasing systems?
Yes, we build the reconciliation logic that joins inspection results, warranty claims, and purchasing records even when those systems have no shared identifier out of the box, typically matching on part number and supplier name combinations validated against real data.
Explore
Related pages
- ServiceCustom Software Development
- IndustryManufacturing software development
- ManufacturingManufacturing ERP Software Development
- Custom Software DevelopmentCustom Construction Software Development
- Custom Software DevelopmentCustom Fintech Software Development
- Custom Software DevelopmentCustom Healthcare Software Development
Insights
Planning guides
- 6 min readHow Much Does Custom CRM Development Cost?Custom CRM development cost typically ranges from $40,000 for a focused pipeline tool to $250,000+ for a multi-team platform with automation and reporting.
- 7 min readCustom Development vs No-Code ToolsCustom development vs no-code tools compared on speed, cost at scale, and where each one actually holds up as your workflow gets more complex.
- 8 min readHow Much Does Custom Software Development Cost?Custom software development cost ranges from $15,000 for a simple internal tool to $500,000 or more for enterprise platforms. Here is what drives the number.
Get an estimate for custom manufacturing software development
Share a few details about your project. A senior engineer reviews every request and replies with next steps, questions, and a rough budget range.